
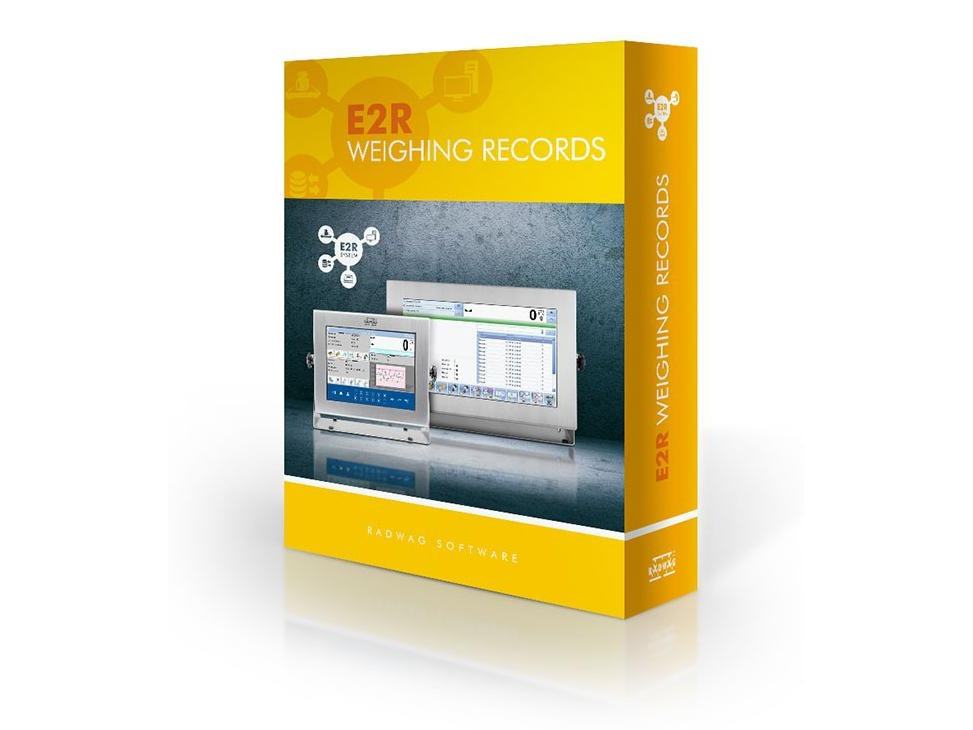
E2R Weighing Records (WX-010-0038)
To be able to analyse and correct them in real time? After all, it is the key to increasing the efficiency of the production line! Our clients, the…
5Y.20.PM
The 5Y.PM balances are more accurate, faster, and more versatile than their predecessors and therefore meet the requirements for equipment used in companies representing various industries. Dosing, formulation-making, and parts counting are just some of the possible applications of these devices. Wherever their potential for impressive accuracy and high load capacity is to be realised, PM balances will prove themselves.
Request a quoteDownload the datasheet
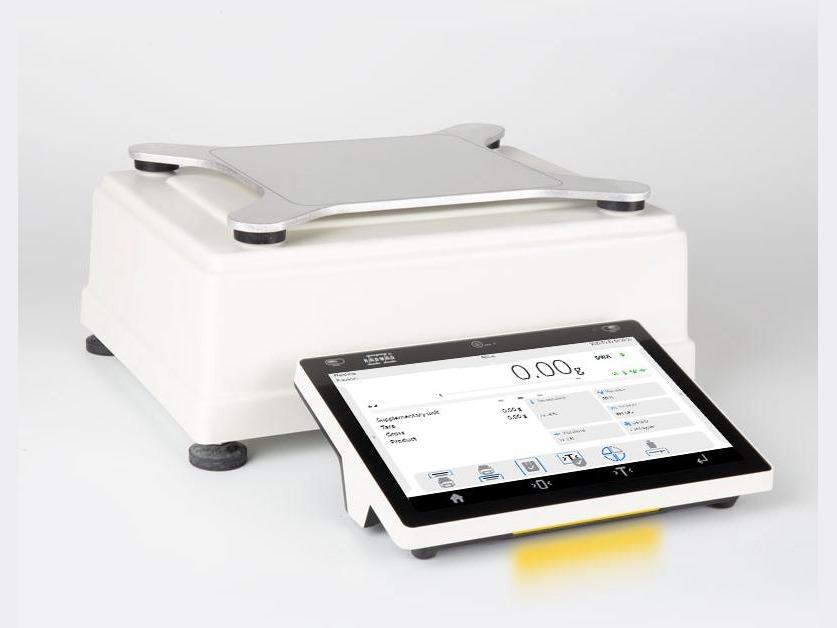
Laboratory Precision Under Industrial Conditions
are the distinguishing features of RADWAG PM balances. All of this is possible thanks to the use of a cutting-edge measuring system based on enhanced
MONO
BLOCK®
technology. The change in the design of the
MONO
BLOCK®
has made it possible to work with a readability of 0.01 g at a maximum capacity of 20 kg and 0.2 g at a maximum capacity of 120 kg, with a repeatability of 0.01 g, and resistance to changes in ambient conditions.
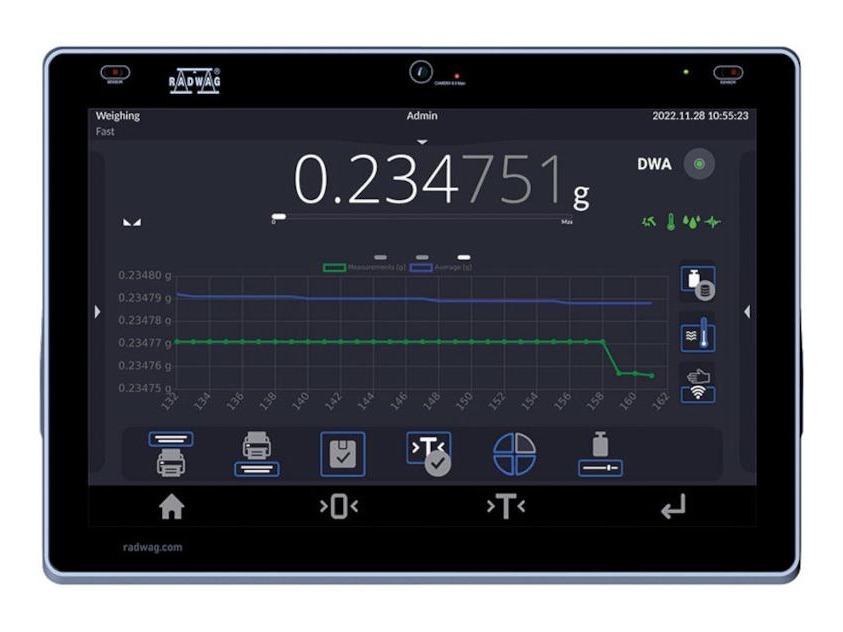
The 5Y.PM balances are more accurate, faster, and more versatile than their predecessors and therefore meet the requirements for equipment used in companies representing various industries. Dosing, formulation-making, and parts counting are just some of the possible applications of these devices. Wherever their potential for impressive accuracy and high load capacity is to be realised, PM balances will prove themselves.
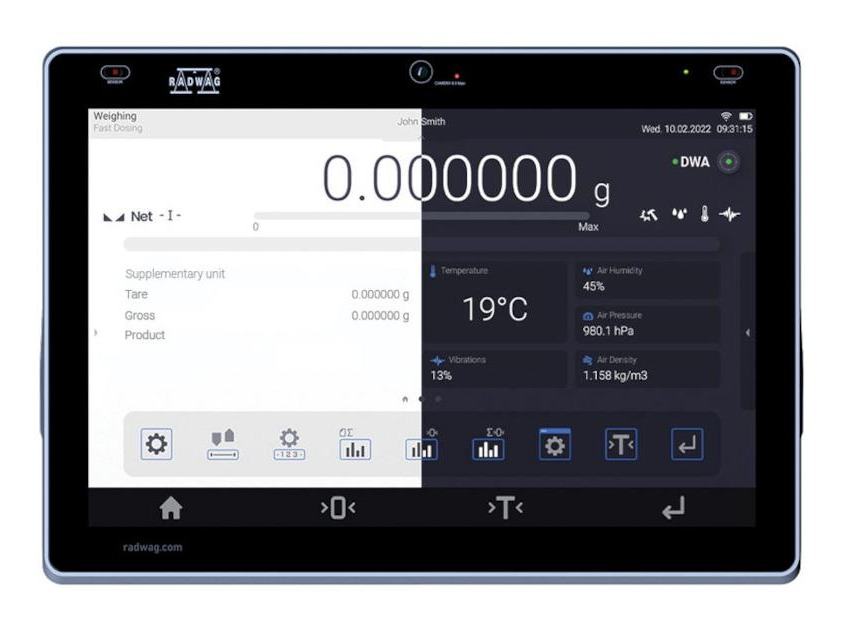
Do you work in the pharmaceutical industry? Do you need a digital signature?
We are offering the laboratory balance which as a standalone fully meets the requirements of 21 CFR Part 11/ EU GMP Annex 11.
- Full data security
- Electronic signatures
- Validations
- Electronic records
- Audit trails
is one of the most popular communication protocols in industrial automation. Implementing it in the 5Y balances and CY10 scales makes the devices of this series friendly to automation integrators.
Under-pan weighing
* RFID ISO/IEC 14443 Type A, 13,56 MHz
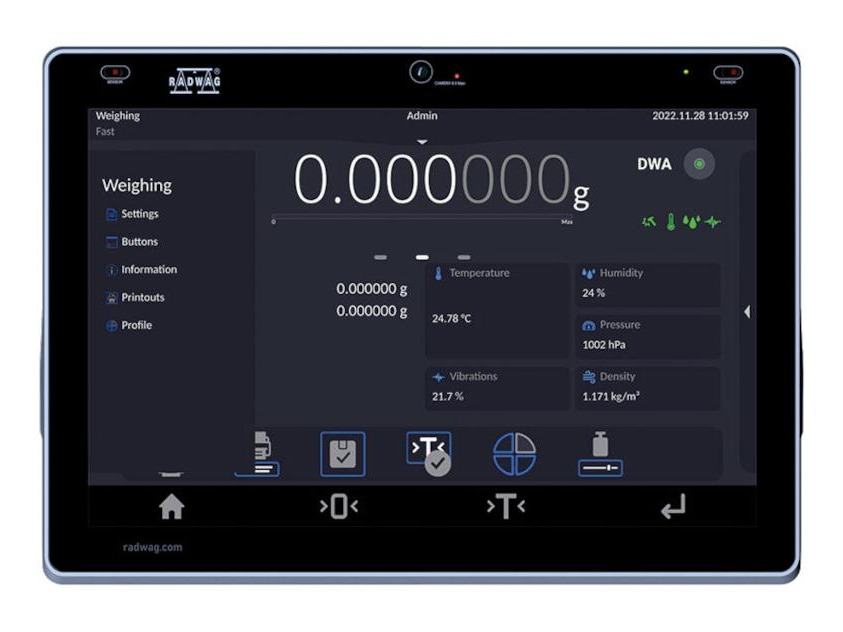
| Maximum capacity [Max] | 20 kg |
|---|---|
| Minimum load | - |
| Readability [d] | 0,01 g |
| Verification unit [e] | - |
| Tare range | -20 kg |
| Minimum weight (USP) | 8,2 g |
| Minimum weight (U=1%, k=2) | 0,82 g |
| Standard repeatability [Max] | 0,015 g |
| Standard repeatability [5% Max] | 0,0041 g |
| Linearity | ±0,03 g |
| Stabilization time | 1 s |
| Adjustment | internal (automatic) |
| OIML Class | - |
| Leveling system | semi-automatic – LevelSENSING |
|---|---|
| Display | 10″ graphic colour touchscreen |
| Delivery components | Precision Balance, weighing pan, fabric dust cover, power supply. |
| Weighing pan dimensions | 200×185 mm |
| Packaging dimensions W x D x H | 520×520×280 mm |
| Net weight | 13,7 kg |
| Gross weight | 16 kg |
| Protection class | IP 43 |
|---|
| Communication interface | 2×USB-A, USB-C, RS 232 (COM3), HDMI, Ethernet, Wi-Fi ® , Hotspot |
|---|
| Power supply | Adapter: 100 – 240V AC 50/60Hz 1A Max; 15V DC 2,4A Balance: 12 – 15V DC 1,4A max; 9 – 17W* |
|---|
| Operating temperature | +10 – +40 °C |
|---|
Diagnostic function aiming at metrological parameters determination (repeatability), the parameters are determined for the actual conditions of use. When speaking of repeatability it may be also used for weighing time optimization. Autotest is operated in an automatic mode thus operator’s time is saved.
Weighing process for which reference mass has been determined together with tolerance for its determination. Dosing tolerance is given in [%] and it is calculated in relation to the reference value thus being a permissible deviation of this process. This solution is used for weighing powders, liquids and loose materials. Dosing function performance is often supported with bargraph - load indicator. For industrial scales it is possible to use a control systems of dosing process.
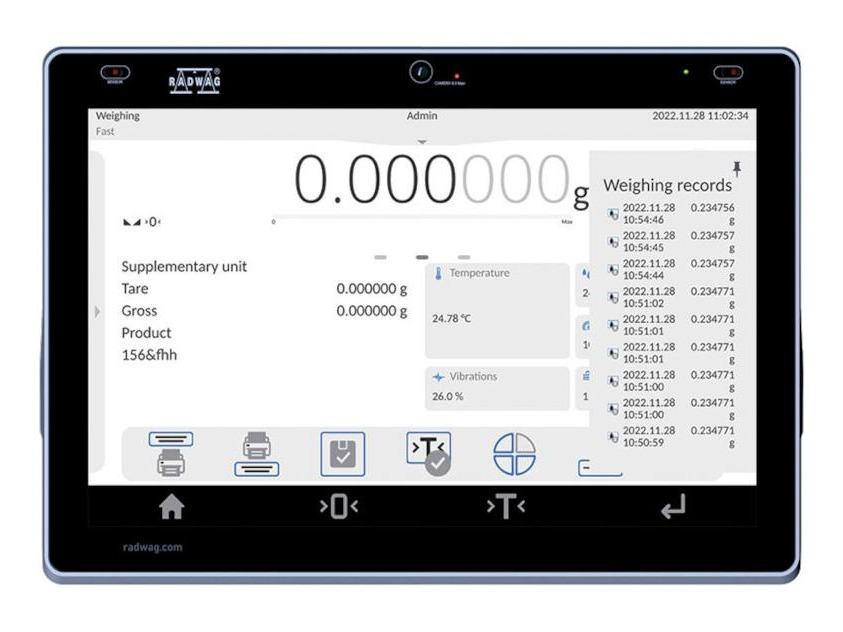
Percent Weighing function is used for comparision of measured products with mass standard. Mass of a mass standard may be a numeric value taken from a database or it may be determined through a measurement process. Each measured product is compared to mass standard, mass of which is presumed as a model 100% ideal mass. For products weighing less than the mass standard, obtained results are lower than 100%, for products weighing more, the obtained results are greatly exceeded.
Function using mass measurement for determination of measured items quantity. Mass of a single item is required for this process. It may be either estimated through weighment or taken from a database. For items counting the following algorithm is used: all items mass / single item mass = quantity. Function operation is supperted by a mechanism of Automatic Correction of Accuracy. This allows to update single item mass in course of the process. To a certain extend Automatic Correction of Accuracy eliminates error which may be a result of different mass values of seemingly alike single elements. For industry solutions items counting may be simultaneously carried out with checkweighing and dosing thus industry solutions feature audio signalling base informing that specified number of items has been weighed. It is possible to apply weighing systems using few platfroms of different MAX capacities and different accuracies.
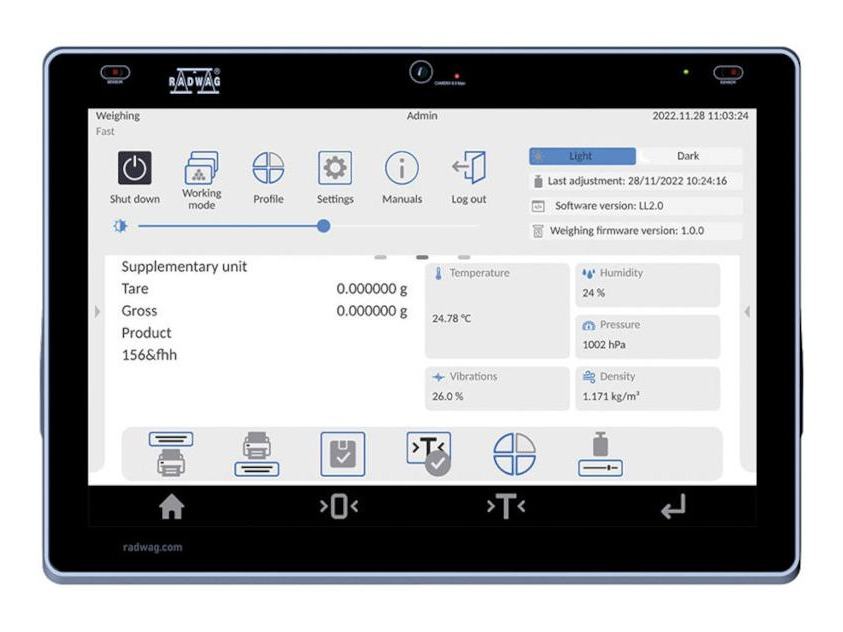
Function registering the greatest temporary indication occurring in course of the weighing process. It is most often used in medical scales in order to hold the measurement indication.
Function supporting the mixture making process, wherein the mixture contains various components. Formulation function usually uses the balance/scale database of components. Formulation serves for monitored checkweighing of every single component with a given tolerance. It is enriched with a set of individual settings.
Statistiscs function registers and analyses performed measurements. This supplies the user withthe following information: Max and Min standard deviation, average value, variance, range et.
Checkweighing function is used for checking whether the measured sample mass is within the predefined threshold values, Low [LO] and Hgh [HI]. The thresholds are given in [g] and [kg] units. Current state of a sample being measured is signalled by means of pictorgams located on a display for laboratory balances, for industrial scales Stackligt System is used. This visual +/- inspection is in operation during segregation, control or packing process of products for which mass has bees determined with a specifaied tolerance, eg. 12860 g ± 5 g
Programmable function supporting the weighing process through control of the following options: sliding weighing chamber doors, printout, zeroing, tarring etc. Especially appreciated wherever preventing the balance from soiling is important.
The solution enables weighing with use of a stand, which is advisable for loads of non-standard shapes and dimensions and those that generate magnetic field.
Diagnostic function allowing to objectively document performed measurements. GLP procedures may be either presented in a short report form or extended one.
Process of mass determination for a product which may unwillingly reposition within the weighing pan. Mass determination in such cases requires much longer period of time when compared to typical weighing process. It is the user who defines period of time needed for control of measured product mass. The user can thus optimize the function depending on the measured product characteristics.
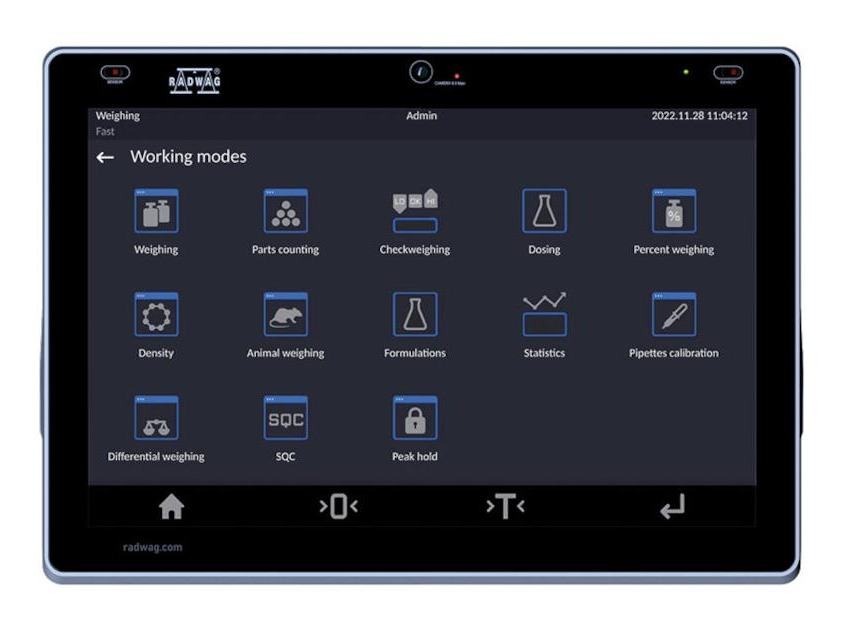
Function verifying correctness of piston pipettes functioning, the verification is performed via gravimetric measurement of the excreted liquid. Pipettes calibration may be either a stand-alone module or it may be operated
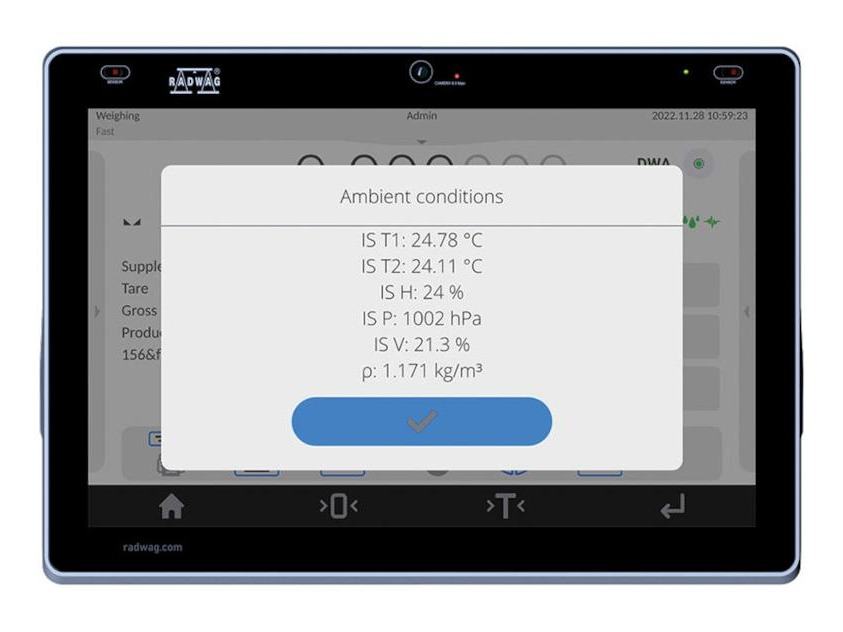
Function performing correction of mass measurement indication, wherein the air density is taken into account. It is used in balances with reading unit < 0,01 mg.
Liquid or solid body density function uses the Archimedes principle and it requires a special kit to be applied. The kit when used, replaces a weighing pan. For solids mass of the sample must be determined first in the air, next in the liquid of specified density. For liquids the so called sinker, density of which has been determined, must be measured first in the air, next in the tested liquid. The density determination process is disturbed by air bubbles which may stick either to the measured sample or the sinker. In case of laboratory equipment very light solids may be measured. For industry, solid bodies density may be determined by means of under-pan weighing. Tested load of significant size may be measured this way.
Differential weighing informs about mass variation a particular sample, wherein the said variation is a result of manufacturing processes.
Differential weighing is often applied in product control process, for which reference product parameters have been specified in order to be used as a source of comparison for the whole series.
Insuchcasestandard deviation is the information which tells about quality and completeness of a final product. For systems based on a feed-back technique such information may be used by control units.
The possibility of cooperation with the THBR 2.0 system
Statistical control for determination of basic statistical criteria: maximum, minimum, standard deviation, mean values for each batch, etc.
Pre-packaged Goods Control mode enables to collect weighings from RADWAG-designed weighing instruments, carry out control and generate PGC reports. Different types of weighing instruments can be combined into a network. The control can be started on a balance or via computer software. It is automatically finished after a respective quantity of packages is verified.
Collected data allows you to assess quality of produced pre-packaged goods and their conformity with:
- internal quality control system;
- 'Pre-Packaged Goods' regulation of 7th May 2009 (Journal of Laws No 91, item 740), on the requirements concerning quantity inspection of pre-packaged goods control, which inspection is to be carried out by means of random selection of the measurements results and sending those results to pre-packaged goods control procedure.
"ALIBI" memory enables saving and storing up to 100000 measurements. Measurements are saved automatically upon each pressing of the key. There is no need for any additional operations or changing settings.
The following data related with the measurements is saved: measurement date; measurement time; result (mass); tare value; operator carrying out the measurement (logged in); product name.
The software saves the measurement in a so called loop, i.e. when the measurement no. 100001 is saved, the measurement 1 gets automatically deleted from the memory.
Measurements saved to balance memory cannot be deleted.
You can preview and print out the data saved to the ALIBI database.
Thanks to wireless communication between the computer and a balance, it is possible to use a balance inside a laminar flow hood and a fume cupboard.
WX-016-0154 RES level: 0,1,2 (PUE HY10)
WX-016-0212 RES level: 0,1,2 (WLY, PUE71)
WX-016-0264 RES level: 0,1,2 (4Y, 5Y)
WX-016-0265 RES level: 0,1,2 (X2, X7)
WX-016-0292 RES level: 0,1,2 (PUE HX7)
WX-016-0293 RES level: 0,1,2 (PUE C32)
WX-001-0133 CFR 21 (4Y, 5Y, CY10)
WX-001-0187 CFR 21 (X2, X7)
The module includes "Audit Trail".
Audit Trail is a kind of a log where all modifications of balance settings, changes in database records and user activity are recorded. Audit Trail, for example, keeps record of previous and new modifications in databases and informs by whom and when they were introduced. This log allows the administrator to track and find out who logged in, when, who signed a document or who used invalid password.
The Audit Trail Reader freeware allows users, upon connection with a balance, to display Audit Trail log and manage it by generating reports of various formats: pdf, xls, csv, html.
Choose the model, probes and accessories. Incompatible combinations are blocked as you go; the remaining rules are checked when the instrument is added to the quote.
Loading the options…
A code can be pasted and the configuration builds itself.
They are quoted separately: the instrument need not be configured.
To be able to analyse and correct them in real time? After all, it is the key to increasing the efficiency of the production line! Our clients, the…
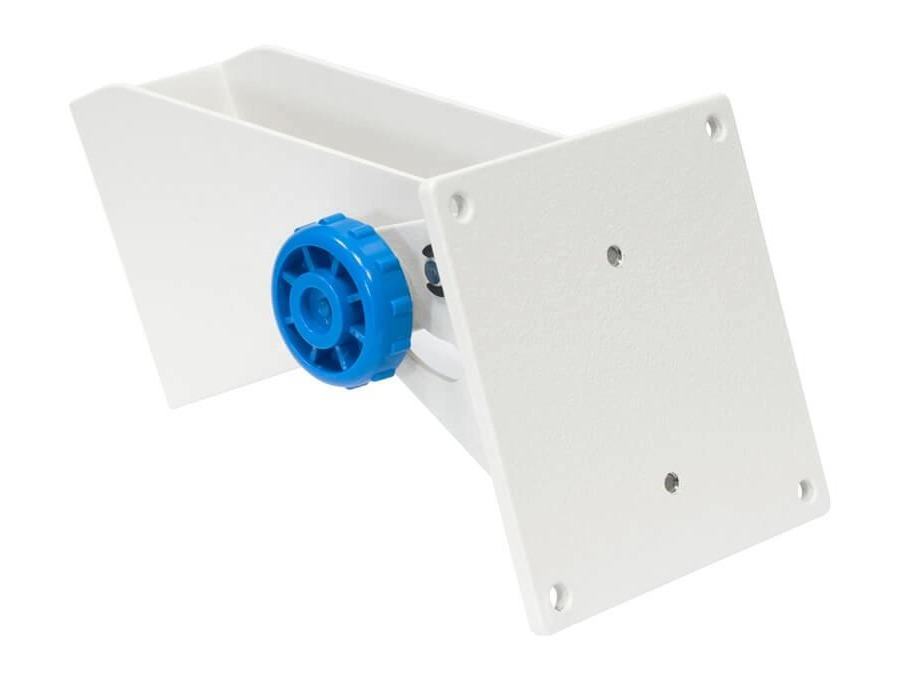
Wall-mounting kit has been designed to facilitate installation of 5Y / PUE CY10 terminals on a vertical surface. The kit enables adjustment of the…
R02 Label Editor is a proprietary application of RADWAG, which allows users to make labels forindustry scales, scales intended for EX area, PGC…
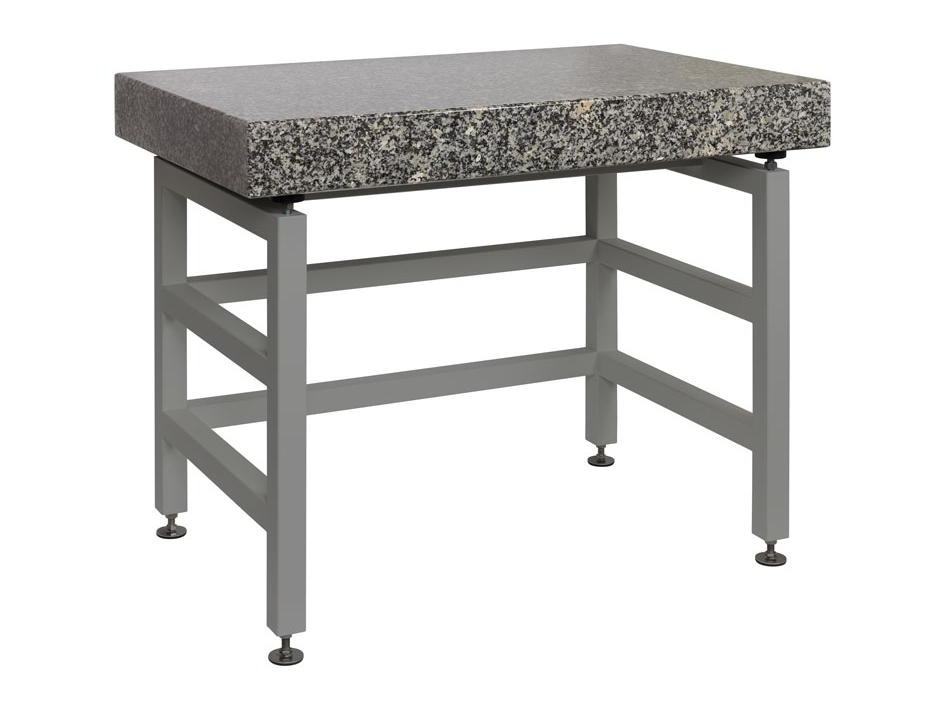
The table has been designed to eliminate ground vibrations during the operation of laboratory equipment such as microbalances, analytical balances…
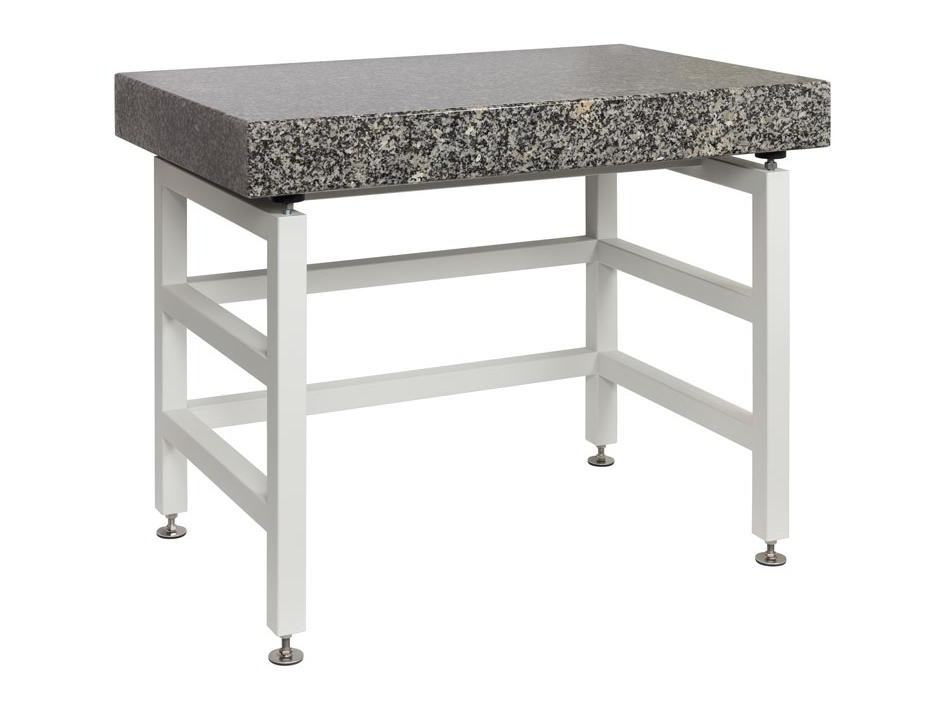
The table has been designed to eliminate ground vibrations during the operation of laboratory equipment such as microbalances, analytical balances…
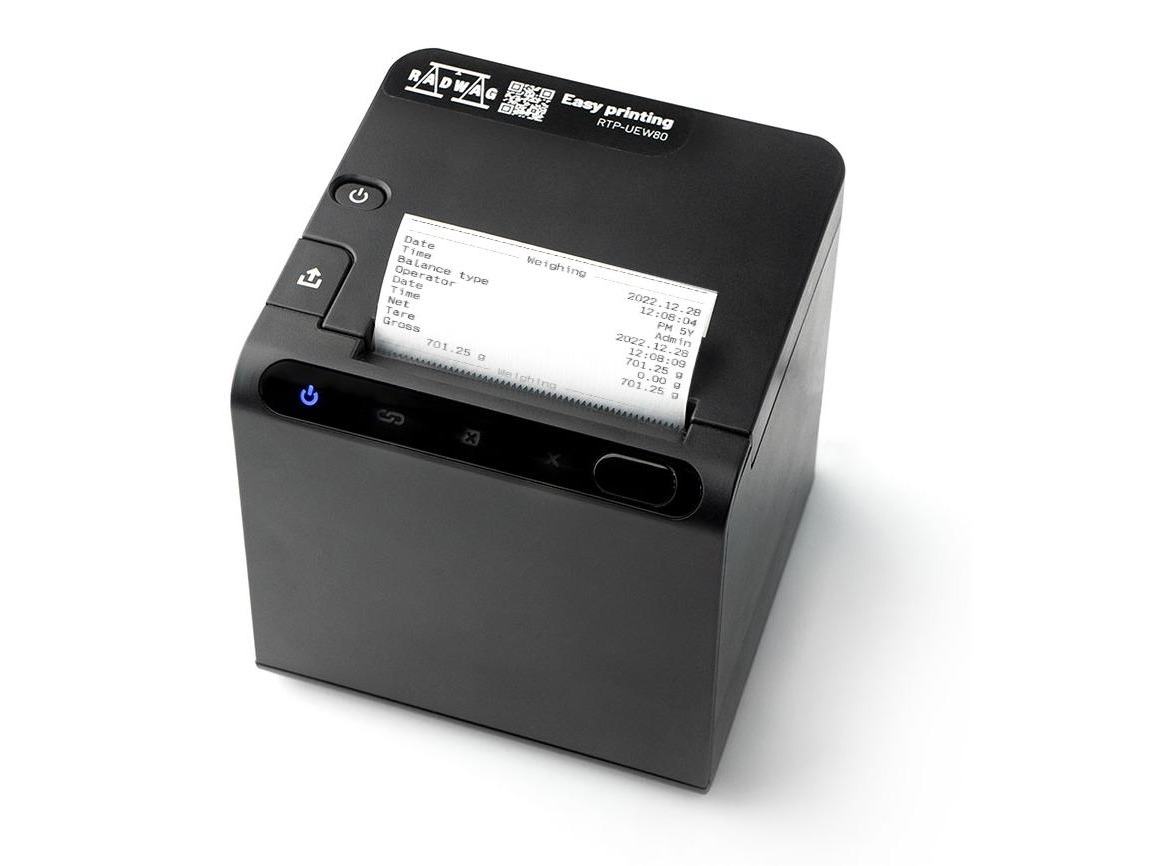
Wireless Wi-Fi® communication is a key advantage of the RADWAG RTP-UEW80 printer. The device enables convenient printing of weighing results…
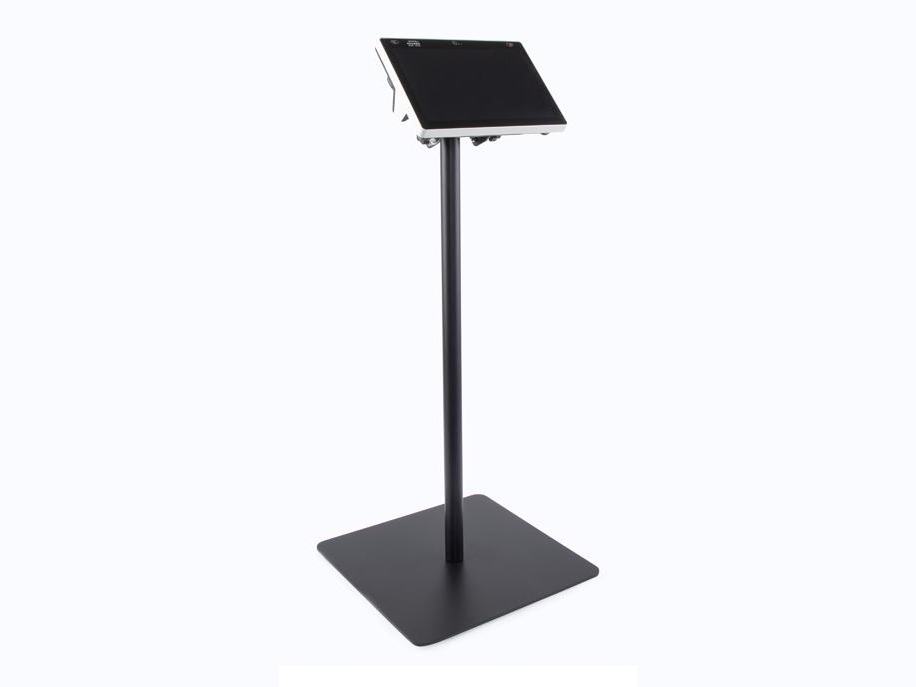
A stand for supporting scale's indicator installed on a cable 5Y / PUE CY10. Mild steel version available.
To be able to analyse and correct them in real time? After all, it is the key to increasing the efficiency of the production line! Our clients, the…
The 21 CFR Part 11 Compliance Module is a solution especially useful for those users who are obliged to conform to provisions of 21 CFR Part 11 and…
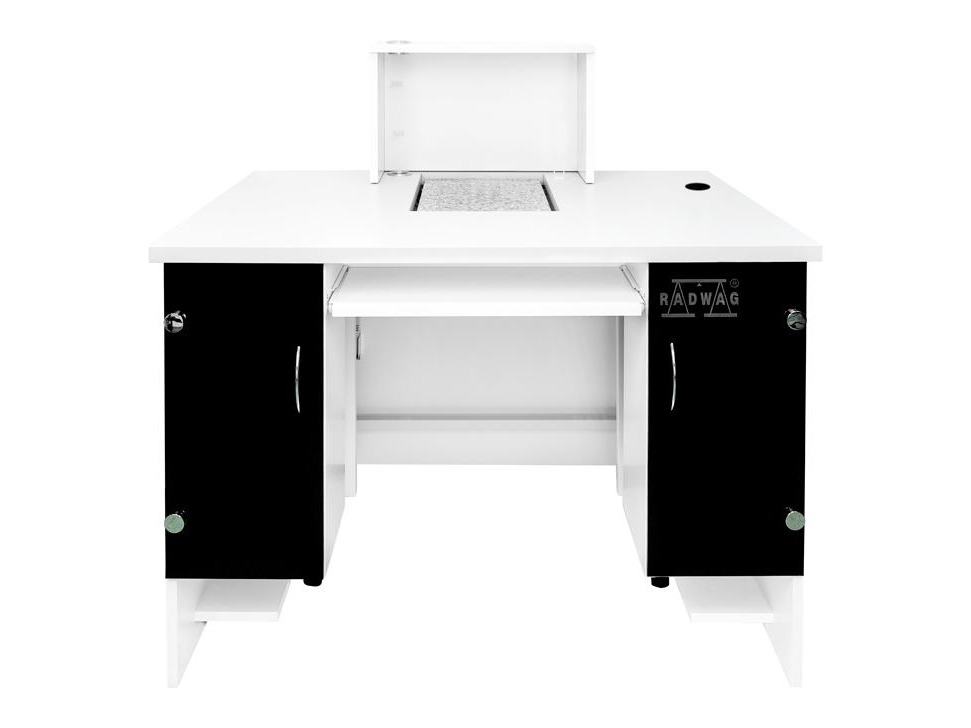
The professional weighing workstation is intended for microbalances and analytical balances. It is equipped with two lockers for a computer and an…
The RADWAG RTP-RU80 is a modern receipt printer designed to work with laboratory and industrial scales. Equipped with RS232 and USB interfaces, it…
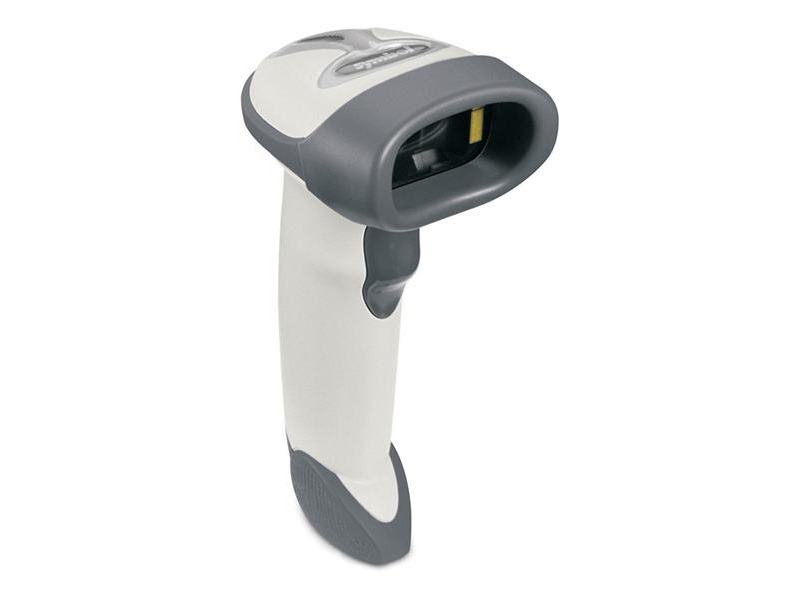
LS2208 barcode scanner is a manual device designed for operation in adverse industrial conditions. It integrates with RADWAG terminals, PUE H315, PUE…
Instruments to quote
No instruments yet. An enquiry can be sent anyway: a specialist answers.