
E2R Weighing (WX-010-0099)
To be able to analyse and correct them in real time? After all, it is the key to increasing the efficiency of the production line! Our clients, the…
PUE HY10
can be supplied from an internal A/C converter (load cell weighing platforms), high resolutions platforms and additional scales and weighing modules.
Request a quoteDownload the datasheet
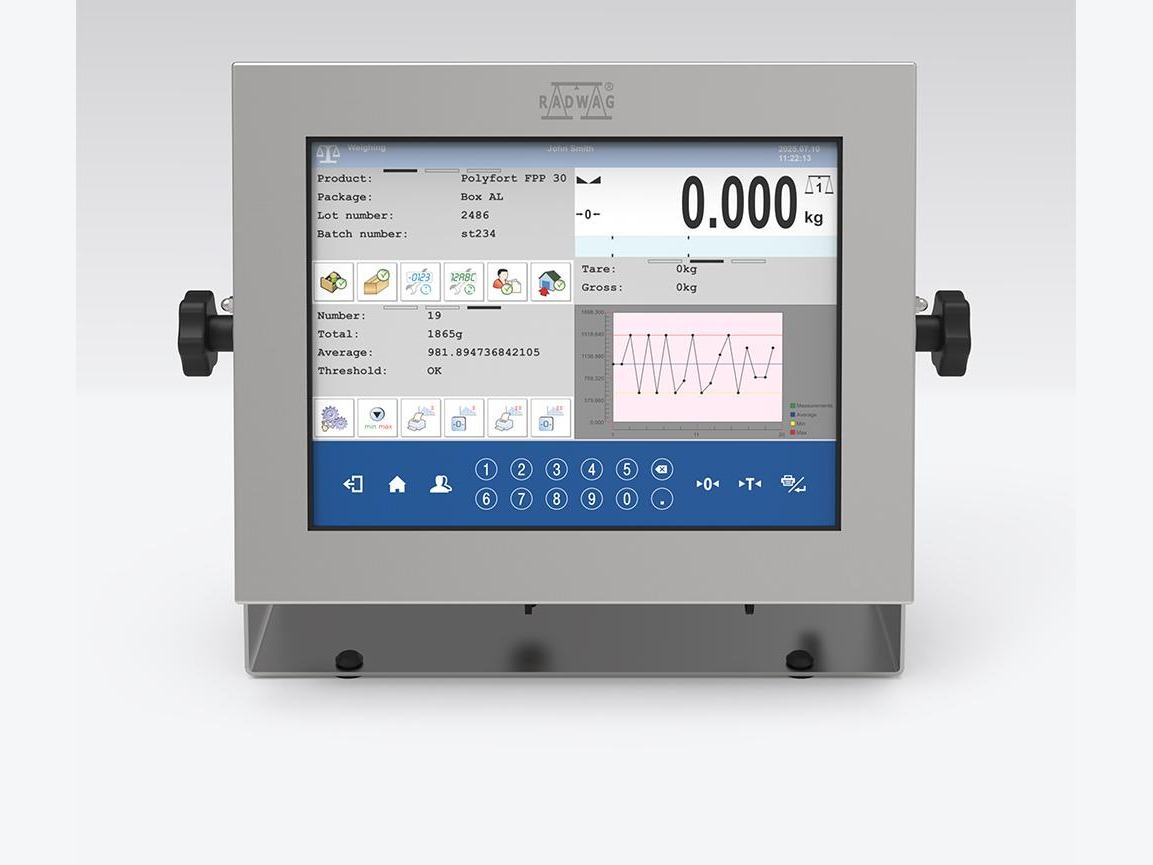
The PUE HY10 is a terminal with extensive functional capabilities. It combines the functions of a weighing indicator for single- and multi-load cell weighing platforms with those of an advanced terminal for collecting, analysing and processing mass measurement results.
can be supplied from an internal A/C converter (load cell weighing platforms), high resolutions platforms and additional scales and weighing modules. Thanks to its rich functionality, a wide range of communication interfaces already in the basic version (with the possibility of expansion), compatibility with many types of weighing platforms and a stainless steel housing with a high degree of protection, the terminal is perfect as the core of multifunctional industrial scales and weighing systems.
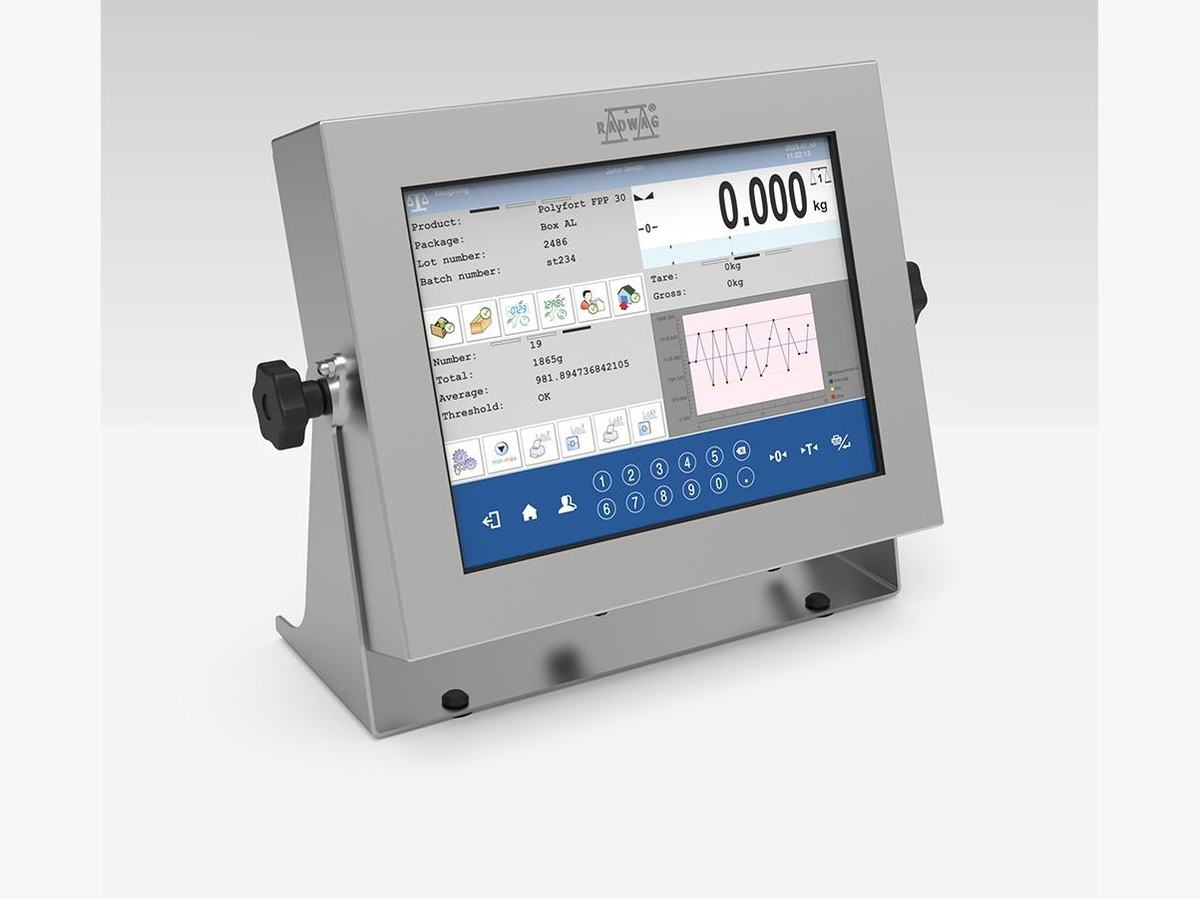
The housing, made of AISI 304 stainless steel, provides a high degree of protection (IP66/67/69) and allows operation in harsh industrial environments with high levels of humidity and dust. It also meets the stringent hygiene requirements of the food and pharmaceutical industries.
The front part of the terminal features a colour graphic display with a diagonal of 10.1’’ and a resolution of 1024x600 pixels, equipped with a capacitive touch panel with additional function and numeric keys. Ease of use, clear menus and intuitive display layout guarantee user comfort.
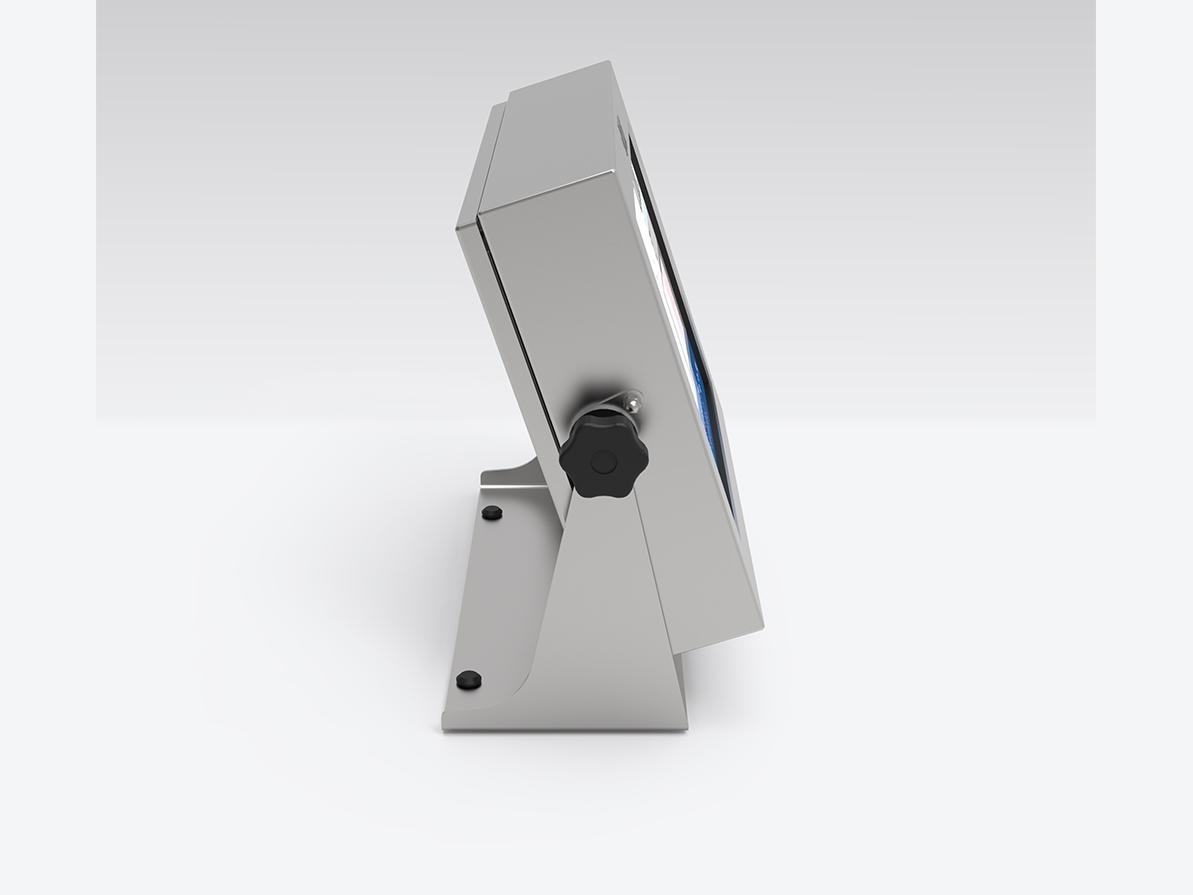
The rear of the housing features sealed communication interface connectors. A stable bracket allows the terminal to be placed on any flat horizontal surface or screwed to a wall and adjusted to the desired angle.
The basic version of the terminal supports one analogue – load cell weighing platform; thanks to the possibility of installing an additional DP-6 module, this number can be increased to two. A maximum of four platforms may be supported – simply connect two more (e.g. high resolution platforms, weighing modules or external scales) using RS232 or TCP/IP digital interfaces.
Extensive software functionality, more than in other RADWAG terminals, allows for complex weighing processes, parts counting, dosing, labelling, formulations, vehicle scale, percent weighing, SQC and PGC.
The information system based on the MySQL database (operators, products, weighings, packaging, formulations, customers, labels, dosing processes and reports) offers extensive possibilities for collecting, processing and sharing data, even with intensive use of the terminal. This makes the terminal an ideal solution for weighing data collection and processing systems used in production processes.
The PUE HY10 terminal software supports cooperation with many peripheral devices such as label printers, barcode readers, transponder card readers, signal columns and external control buttons, enabling their flexible configuration. The modifiable display workspace allows the user to organise the displayed information, bar graphs, buttons and graphics according to their needs.
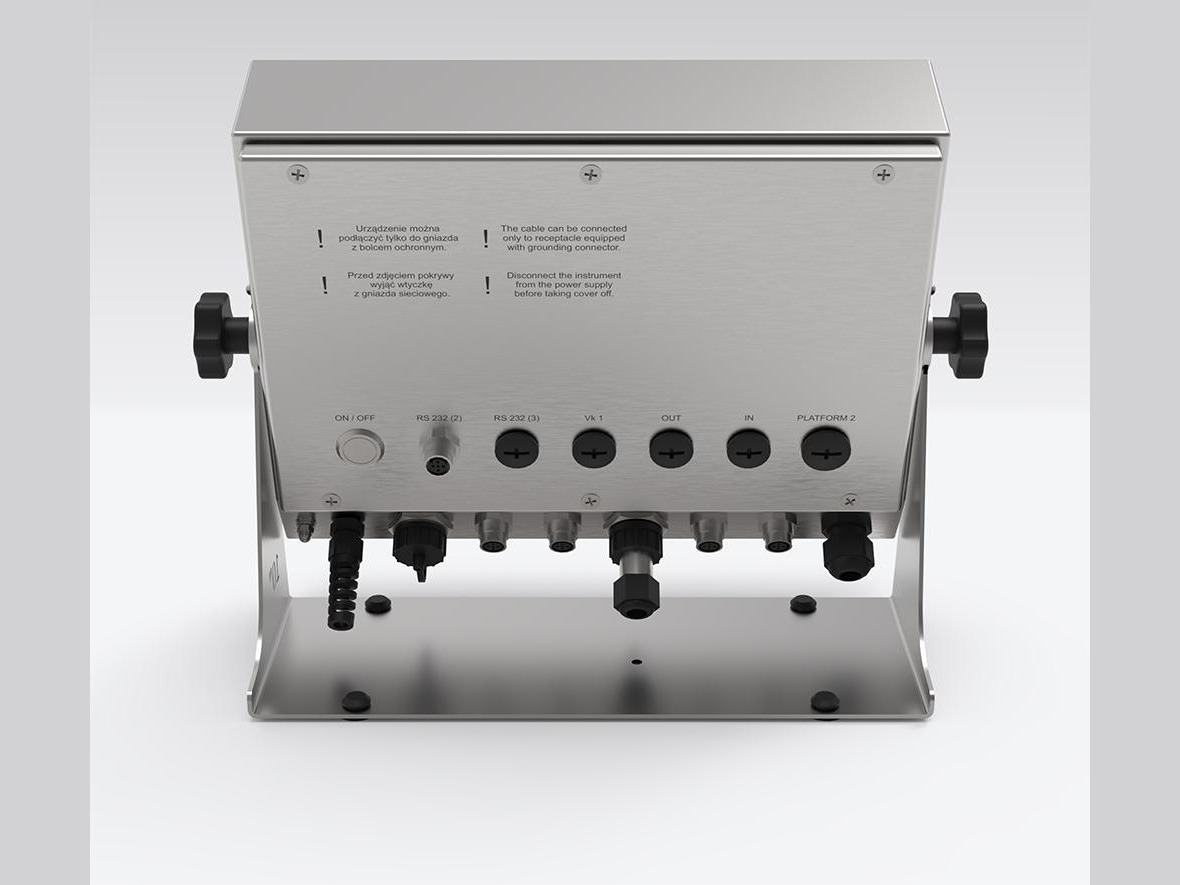
The standard version of the terminal is equipped with RS232, USB, Ethernet and digital input/output interfaces, as well as the following communication protocols: CBCP-03 character communication protocol and Modbus TCP/IP. The range of interfaces can be expanded with RS485, analogue outputs (4-20mA, 0-20mA, 0-10V), additional 12 inputs/outputs and Wi-Fi®, as well as PROFIBUS, PROFINET and Ethernet/IP protocols. Communication interfaces allow cooperation with many external devices, automatic regulation and control systems, and superior IT systems.
Stainless Steel in RADWAG products
Learn about the use and maintenance of stainless steel products:
Stainless Steel in RADWAG products. Standard and special applications
Wi-Fi® is a registered trademark of Wi-Fi Alliance®.
| OIML Class | II or III |
|---|---|
| Maximum quantity of verification units | 6000 e |
| Minimum volatge per verification unit | 0,4 µV |
| Maximum voltage per verification unit | 3,25 µV |
| Minimum load cell impedance | 50 Ω |
| Maximum load cell impedance | 1200 Ω |
| Load cell excitation voltage | 5V DC |
| Maximum increase of signal | 19,5 mV |
| Connection of load cells | 4 or 6 wires + shield |
| Display | 10,1″ graphic colour touchscreen |
|---|---|
| Device dimensions W x D x H | 357×275×120 mm |
| Packaging dimensions W x D x H | 420×350×230 mm |
| Net weight | 5,7 kg |
| Gross weight | 7 kg |
| Protection class | IP 66 / 67 / 69 |
|---|---|
| Touch panel | capacitive |
| Keypad | touch screen |
| Housing | Stainless steel |
| Communication interface | 2×RS232, 2×USB-A, Ethernet, 4 IN / 4 OUT (digital) |
|---|---|
| Optional interfaces | module Wi-Fi ® 802.11 b/g/n, module Profibus (DP SLAVE), module RS485, module PROFINET (RJ45), analog output module (4-20mA, 0-20mA, 0-10V) , 12IN / 12OUT (IN – 5-24 VDC, OUT – max 30 VDC, 0,5 ADC) |
| Operating temperature | -10 – +40 °C |
|---|---|
| Relative humidity | 10% – 85% RH no condensation |
| Operating system | Linux |
|---|---|
| Processor | quad-core 64-bit Cortex-A53 1,2 GHz |
| Memory | RAM 1GB LPDDR2 |
| Data memory | 16 GB (micro SD) |
| Max number of platforms | 4 |
Weighing process for which reference mass has been determined together with tolerance for its determination. Dosing tolerance is given in [%] and it is calculated in relation to the reference value thus being a permissible deviation of this process. This solution is used for weighing powders, liquids and loose materials. Dosing function performance is often supported with bargraph - load indicator. For industrial scales it is possible to use a control systems of dosing process.
Marking products with the right symbols contributes to quick and reliable identification. The balance/scale usually transfers product mass or product quantity to the label printer. The transferred value is printed with the following information: bar code, pictogram, content, address etc. In laboratory the labelling is performed in a semi-automatic mode, for industry in an automatic one (dynamic scales).
Control of sample's mass carried out with reference to specified MIN and MAX thresholds. The weight is considered to be correct if it is comprised within threshold values. A graphic visualisation of weighing result is displayed in a form of a bar graph.
Percent Weighing function is used for comparision of measured products with mass standard. Mass of a mass standard may be a numeric value taken from a database or it may be determined through a measurement process. Each measured product is compared to mass standard, mass of which is presumed as a model 100% ideal mass. For products weighing less than the mass standard, obtained results are lower than 100%, for products weighing more, the obtained results are greatly exceeded.
Function adding new mass value to already obtained one. This allows to determine mass content of the mixture, being a composition of number of different consistence components. Totalizing is limited by maximum capacity parameter.
Function using mass measurement for determination of measured items quantity. Mass of a single item is required for this process. It may be either estimated through weighment or taken from a database. For items counting the following algorithm is used: all items mass / single item mass = quantity. Function operation is supperted by a mechanism of Automatic Correction of Accuracy. This allows to update single item mass in course of the process. To a certain extend Automatic Correction of Accuracy eliminates error which may be a result of different mass values of seemingly alike single elements. For industry solutions items counting may be simultaneously carried out with checkweighing and dosing thus industry solutions feature audio signalling base informing that specified number of items has been weighed. It is possible to apply weighing systems using few platfroms of different MAX capacities and different accuracies.
Function registering the greatest temporary indication occurring in course of the weighing process. It is most often used in medical scales in order to hold the measurement indication.
Function supporting the mixture making process, wherein the mixture contains various components. Formulation function usually uses the balance/scale database of components. Formulation serves for monitored checkweighing of every single component with a given tolerance. It is enriched with a set of individual settings.
Statistiscs function registers and analyses performed measurements. This supplies the user withthe following information: Max and Min standard deviation, average value, variance, range et.
Checkweighing function is used for checking whether the measured sample mass is within the predefined threshold values, Low [LO] and Hgh [HI]. The thresholds are given in [g] and [kg] units. Current state of a sample being measured is signalled by means of pictorgams located on a display for laboratory balances, for industrial scales Stackligt System is used. This visual +/- inspection is in operation during segregation, control or packing process of products for which mass has bees determined with a specifaied tolerance, eg. 12860 g ± 5 g
Diagnostic function allowing to objectively document performed measurements. GLP procedures may be either presented in a short report form or extended one.
Process of mass determination for a product which may unwillingly reposition within the weighing pan. Mass determination in such cases requires much longer period of time when compared to typical weighing process. It is the user who defines period of time needed for control of measured product mass. The user can thus optimize the function depending on the measured product characteristics.
Differential weighing informs about mass variation a particular sample, wherein the said variation is a result of manufacturing processes.
Differential weighing is often applied in product control process, for which reference product parameters have been specified in order to be used as a source of comparison for the whole series.
Insuchcasestandard deviation is the information which tells about quality and completeness of a final product. For systems based on a feed-back technique such information may be used by control units.
Weight function to change the weight unit.
Statistical control for determination of basic statistical criteria: maximum, minimum, standard deviation, mean values for each batch, etc.
"ALIBI" memory enables saving and storing up to 100000 measurements. Measurements are saved automatically upon each pressing of the key. There is no need for any additional operations or changing settings.
The following data related with the measurements is saved: measurement date; measurement time; result (mass); tare value; operator carrying out the measurement (logged in); product name.
The software saves the measurement in a so called loop, i.e. when the measurement no. 100001 is saved, the measurement 1 gets automatically deleted from the memory.
Measurements saved to balance memory cannot be deleted.
You can preview and print out the data saved to the ALIBI database.
Complex weighing mode for registration of weighings that are part of transactions such as sale, purchase and warehouse transfer. You can create a new transaction using the scale. It is possible to pause the transaction or abort it. The function supports warehouse management in an enterprise.
WX-016-0152 Audit Trail (PUE HY10)
WX-016-0201 Audit Trail (PUE 7.1, PUE 7.1P)
WX-016-0210 Audit Trail (WLY)
Audit Trail is a kind of a log where all modifications of balance settings, changes in database records and user activity are recorded. Audit Trail, for example, keeps record of previous and new modifications in databases and informs by whom and when they were introduced.
The Audit Trail Reader freeware allows users, upon connection with a balance, to display Audit Trail log and manage it by generating reports of various formats: pdf, xls, csv, html.
WX-016-0208 Workflow (PUE HY10)
Workflowis an additional module that enables developing a path of a customized weighing process adapted to individual requirements of a particular production process. Easy-to-operate and intuitive interface allows to create an algorithm of operation and send it to a weighing instrument compatible with the software. Workflow can be assigned to operators, products, formulations, formulation ingredients, it is possible to store it in a database.
WX-016-0153 RDA (PUE HY10)
RADWAG Data Access (RDA) module enables integration of weighing instruments, based onHY10 and PUE 7.1 terminal, with customers’ IT systems. The module has to be unlocked with a license key (Setup/Misc./Extensions module/RDA data access module). The activation must proceed in accordance with the instructions displayed on the indicator. Communication is carried out via WebSocket and all data has to be sent as JavaScript Object Notation (JSON). Data can be sent from customer system to the weighing instrument (databases - products, customers, operators, etc.) and the other way around (reports - weighings).
WX-016-0154 RES level: 0,1,2 (PUE HY10)
WX-016-0212 RES level: 0,1,2 (WLY, PUE71)
WX-016-0264 RES level: 0,1,2 (4Y, 5Y)
WX-016-0265 RES level: 0,1,2 (X2, X7)
WX-016-0292 RES level: 0,1,2 (PUE HX7)
WX-016-0293 RES level: 0,1,2 (PUE C32)
Character communication protocol is designed for communication between RADWAG balance and external device via RS232, Ethernet or Wi-Fi®®* interfaces. The protocol consists of commands sent from the external device to the balance and responses sent from the balance to the device. Responses are sent from the balance each time a command is received as a response to the command. The commands that make up the communication protocol allow you to obtain information about the status of the balance and ways to influence its operation, for example, they allow you to receive weighing results from the balance, control the display, etc.
To be able to analyse and correct them in real time? After all, it is the key to increasing the efficiency of the production line! Our clients, the…
To be able to analyse and correct them in real time? After all, it is the key to increasing the efficiency of the production line! Our clients, the…
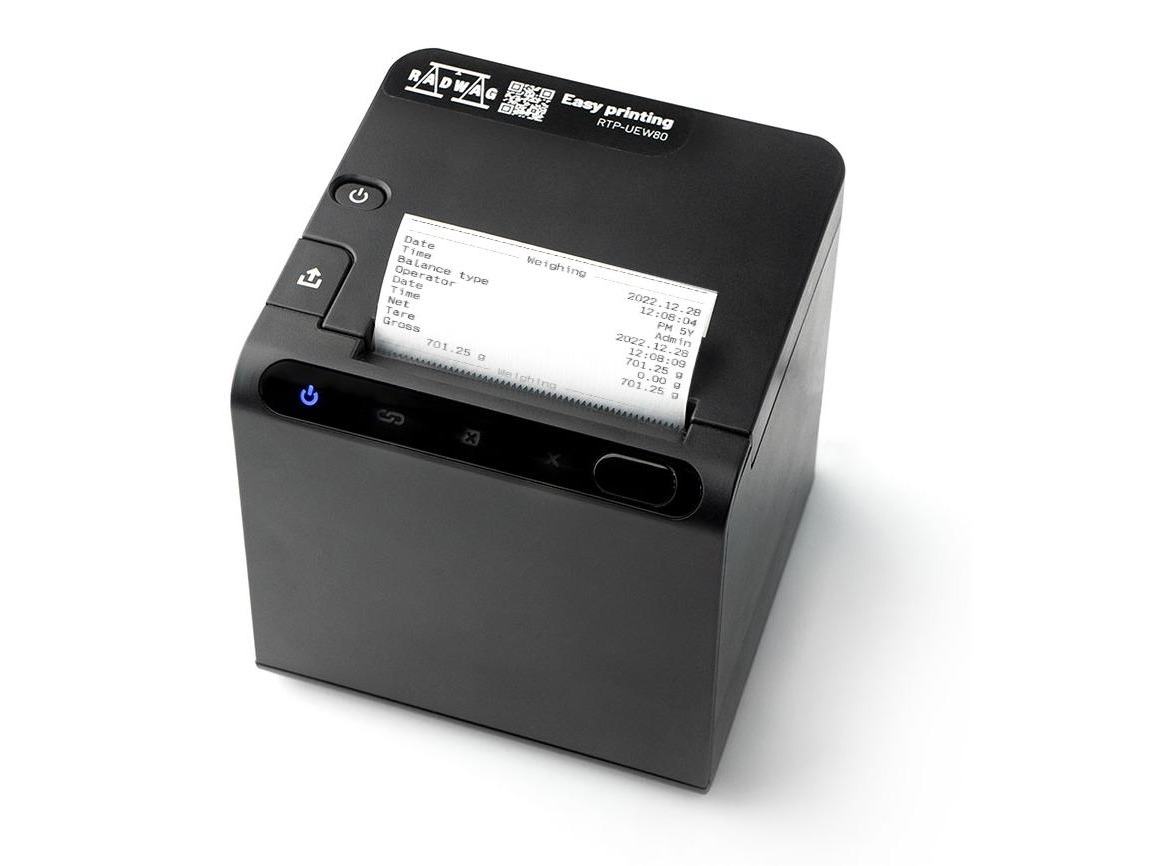
Wireless Wi-Fi® communication is a key advantage of the RADWAG RTP-UEW80 printer. The device enables convenient printing of weighing results…
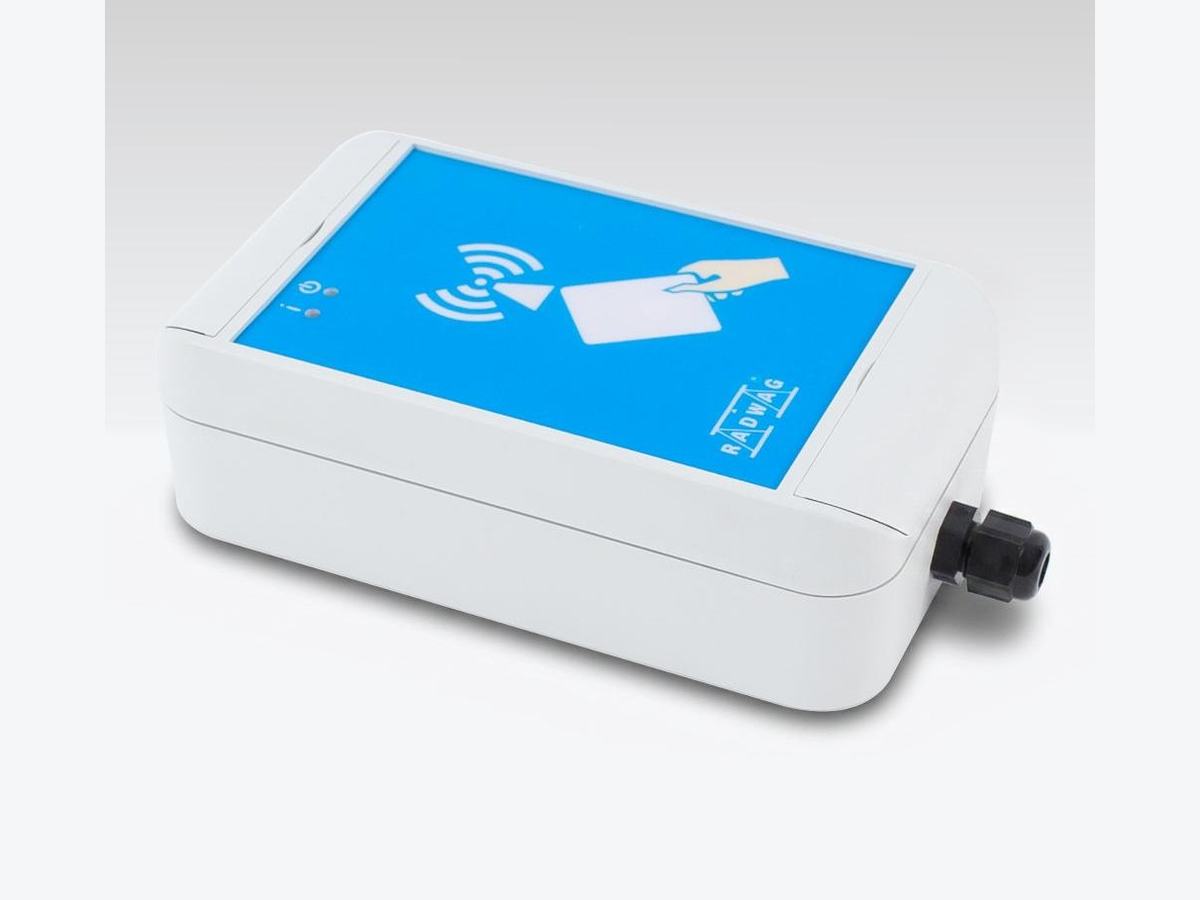
The CK-02/3 is additional equipment for load cell based industrial scales. It can be used for:
Character communication protocol is designed for communication between RADWAG balance and external device via RS232, Ethernet or Wi-Fi®* interfaces.
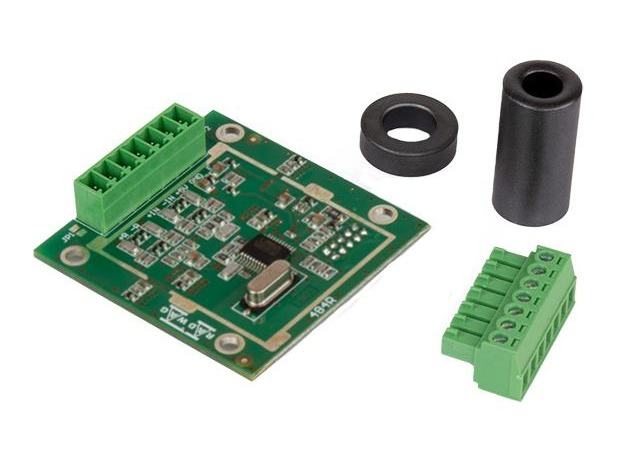
Enhance the functionality of your weighing system with the DP-6 module from RADWAG, a leader in precision weighing innovations. This advanced module…
R02 Label Editor is a proprietary application of RADWAG, which allows users to make labels forindustry scales, scales intended for EX area, PGC…
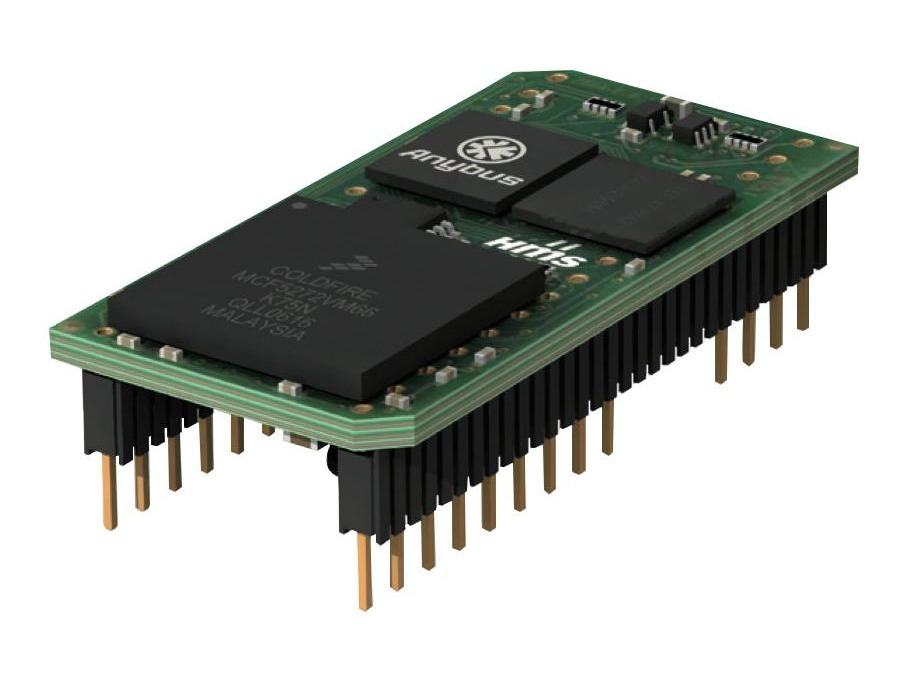
EtherNet/IP - (Ethernet Industrial Protocol), an industrial communication protocol using Ethernet. EtherNet/IP is based on CIP (Common Industrial…
The RADWAG RTP-RU80 is a modern receipt printer designed to work with laboratory and industrial scales. Equipped with RS232 and USB interfaces, it…
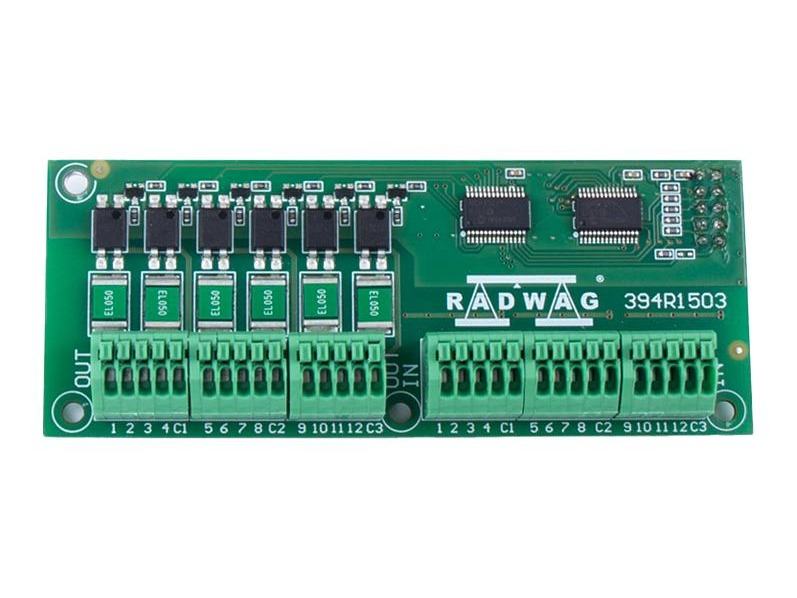
IN/OUT module – semiconductor digital inputs/outputs which can take two binary states: “0” (inactive) or “1” (active). The input ativation performs…
Profinet– an open communication system based on the industrial Ethernet standard. It is a certain combination of features of PROFIBUS DB standard and…
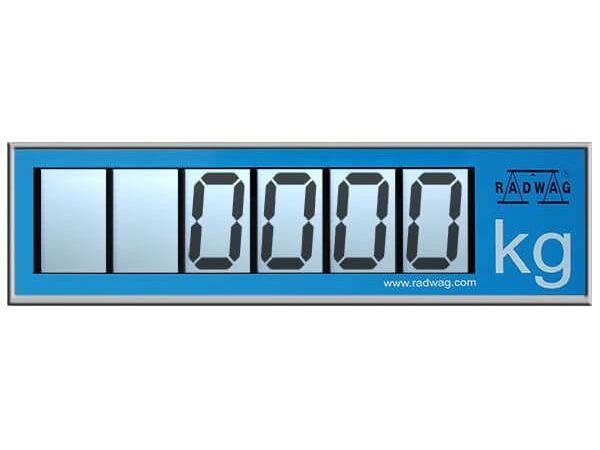
Large-size additional display is an accessory of load-cell scales.
Instruments to quote
No instruments yet. An enquiry can be sent anyway: a specialist answers.